Northern Manufacturing fabricates custom, non-catalog stainless and specialty-alloy tanks directly from your engineering drawings at our Oak Harbor, Ohio facility: one-off and low-series 316L stainless steel storage tanks, duplex 2205 and 2507 process tanks, and AL-6XN and Hastelloy C-276/C-22 chemical tanks. Shells are rolled in-house in one piece where the geometry allows, seams are welded by 60+ AWS-certified welders under ASME BPVC Section IX and AWS D1.6 qualified procedures, and wetted surfaces are pickled and passivated to ASTM A380 and A967 on request in our 55-foot spray booth before shipment.
ISO 9001:2015 certified by AVU Registrations (IAS-accredited, certificate #00157-4). AWS Certified Welding Inspector (CWI) on staff and ASNT SNT-TC-1A Level III NDE capability in-house. Stainless tank work runs inside our 40,000 sq ft dedicated stainless-only production space, with carbon and aluminum in separate bays, so free iron never reaches a product-contact surface.
Project Fit: Custom Build-to-Print vs. Out of Scope
We focus on custom, customer-engineered tanks where heavy plate, tight dimensional tolerances, or corrosion-resistant alloys rule out catalog tank suppliers:
| Fit | Scope Details |
|---|---|
| What we build | Customer-engineered one-off and low-series tanks built from your drawings in 304L, 316L, duplex 2205/2507, AL-6XN, and Hastelloy C-276/C-22; large, heavy-wall, rectangular, or conical geometries; one-piece rolled shells, full-penetration welds, and in-house 55-foot pickling. |
| What we do not offer | Stock or catalog tanks, high-volume commodity production runs, standalone tank design or PE engineering services, field-erected storage tanks, or R-stamp vessel repairs (we do not hold the R stamp). |
What We Build
A tank is often the simplest drawing in a project package and the most expensive weldment to get wrong, because everything it holds contacts every weld:
Storage and Process Tanks
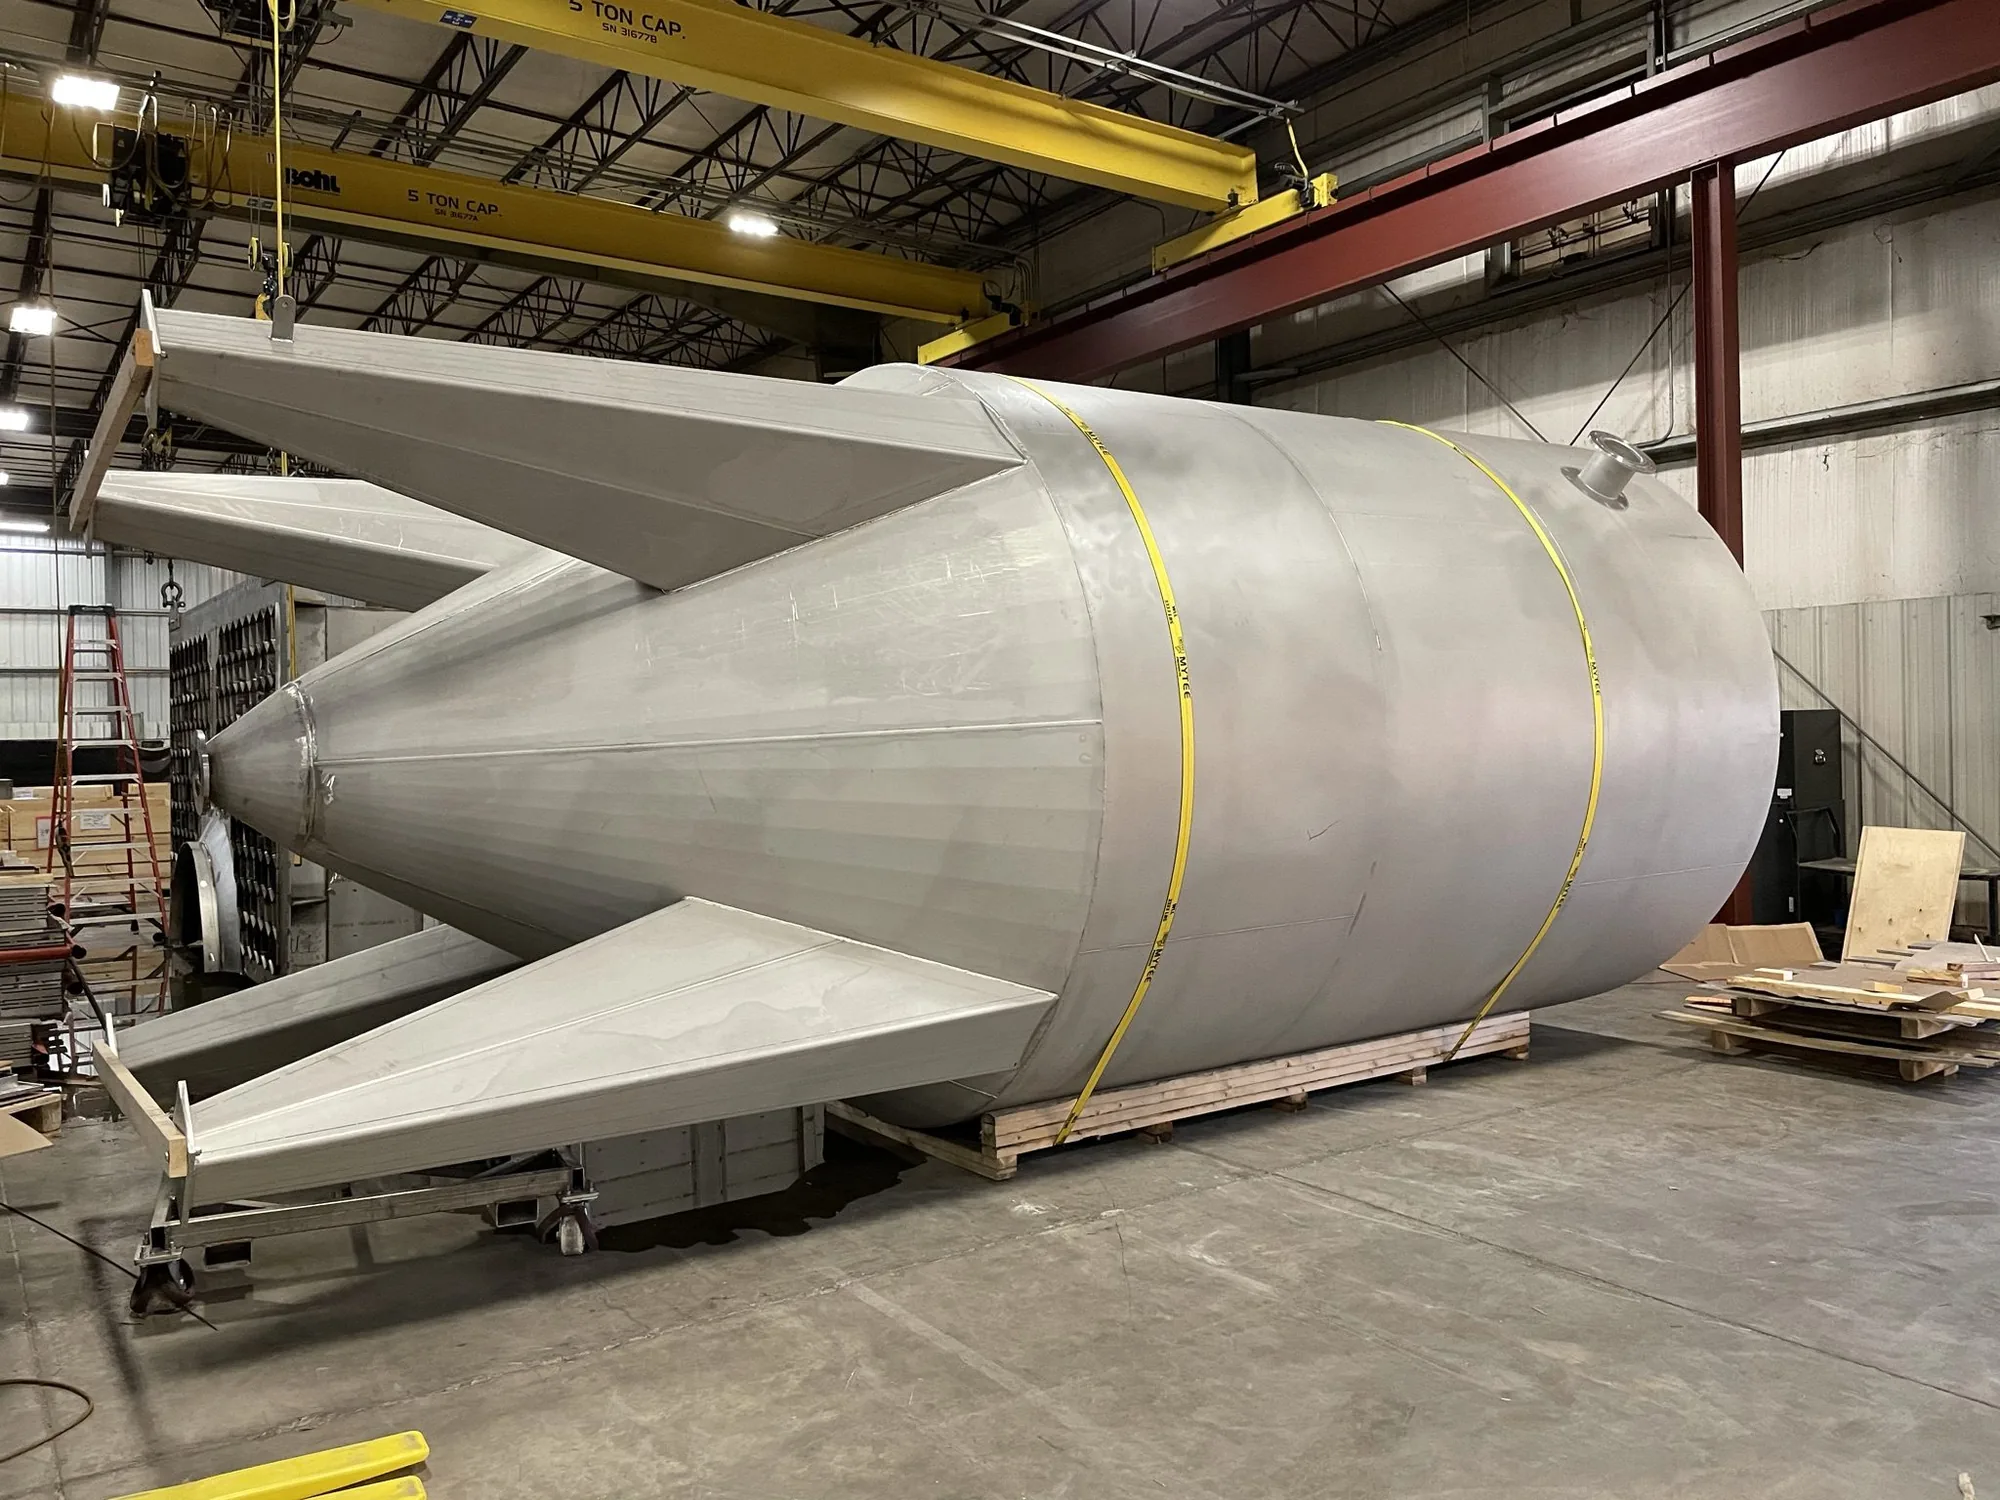
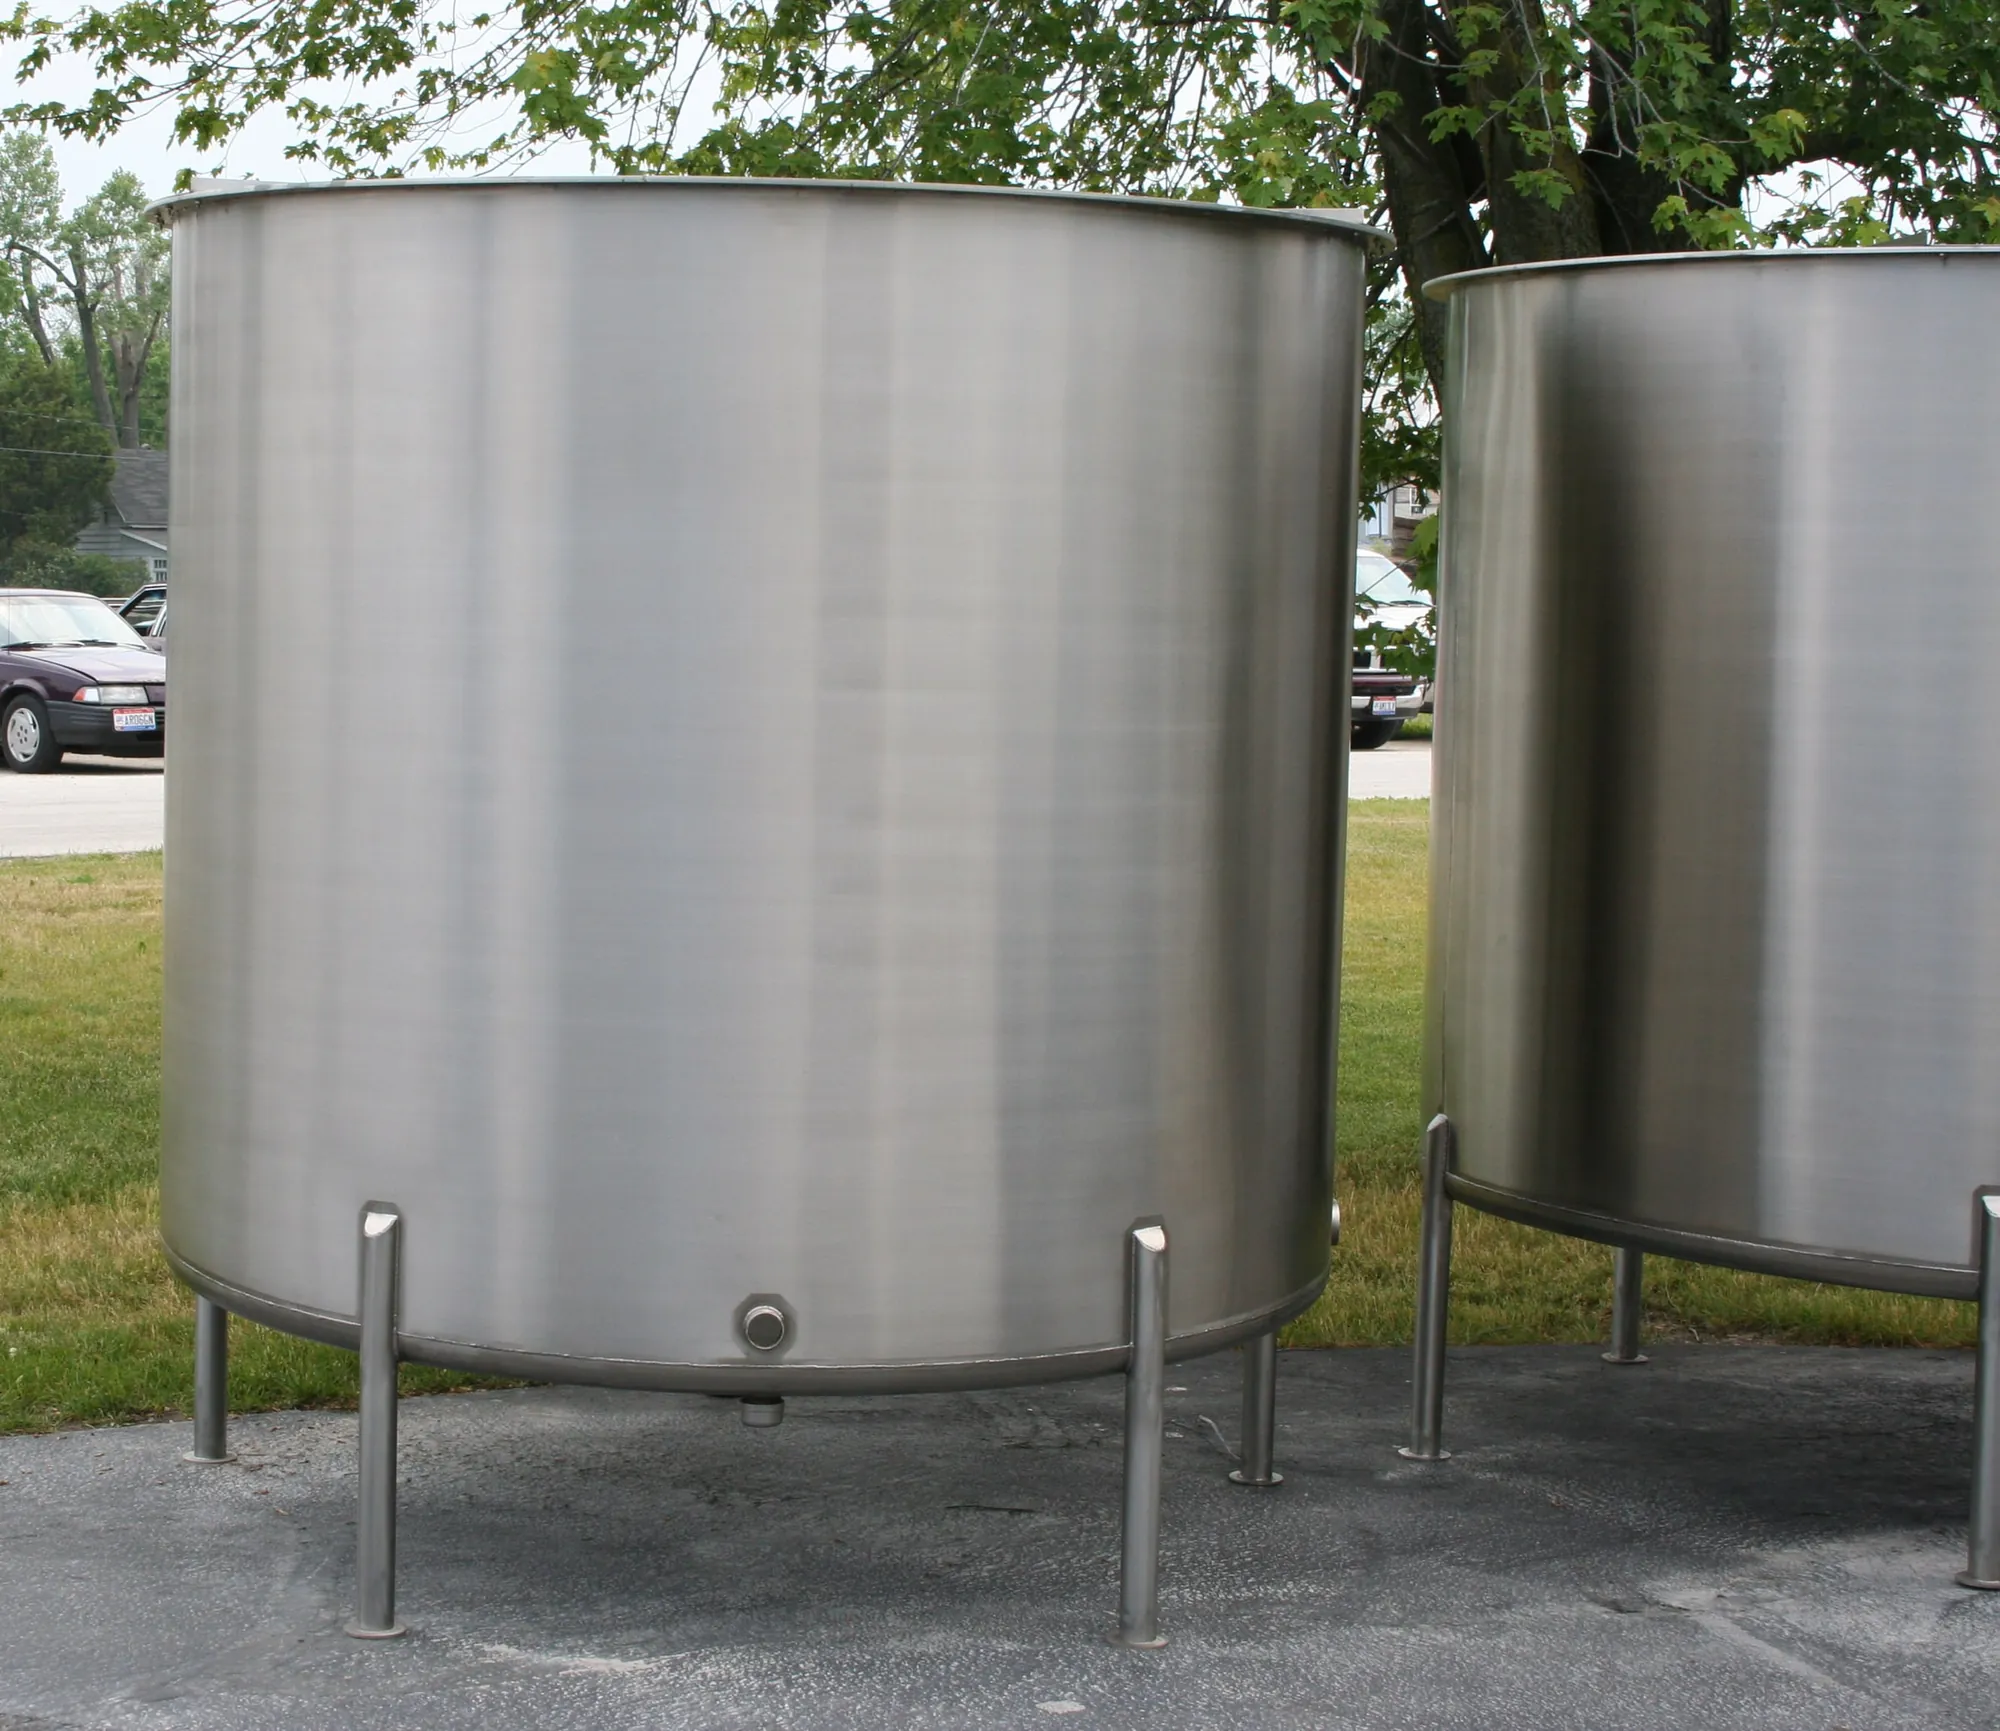
Vertical and horizontal vessels for water, wastewater, chemical, and industrial service, including custom 316L storage tanks and AL-6XN or duplex chemical storage tanks, with shells rolled in one piece where the geometry allows so there are fewer seams to inspect and clean. Nozzles, manways, legs, and lifting lugs fit to the model and weld to qualified procedures, with ASME U Stamp (#63199) pressure vessel construction available when specified.
Mixing and Blending Tanks
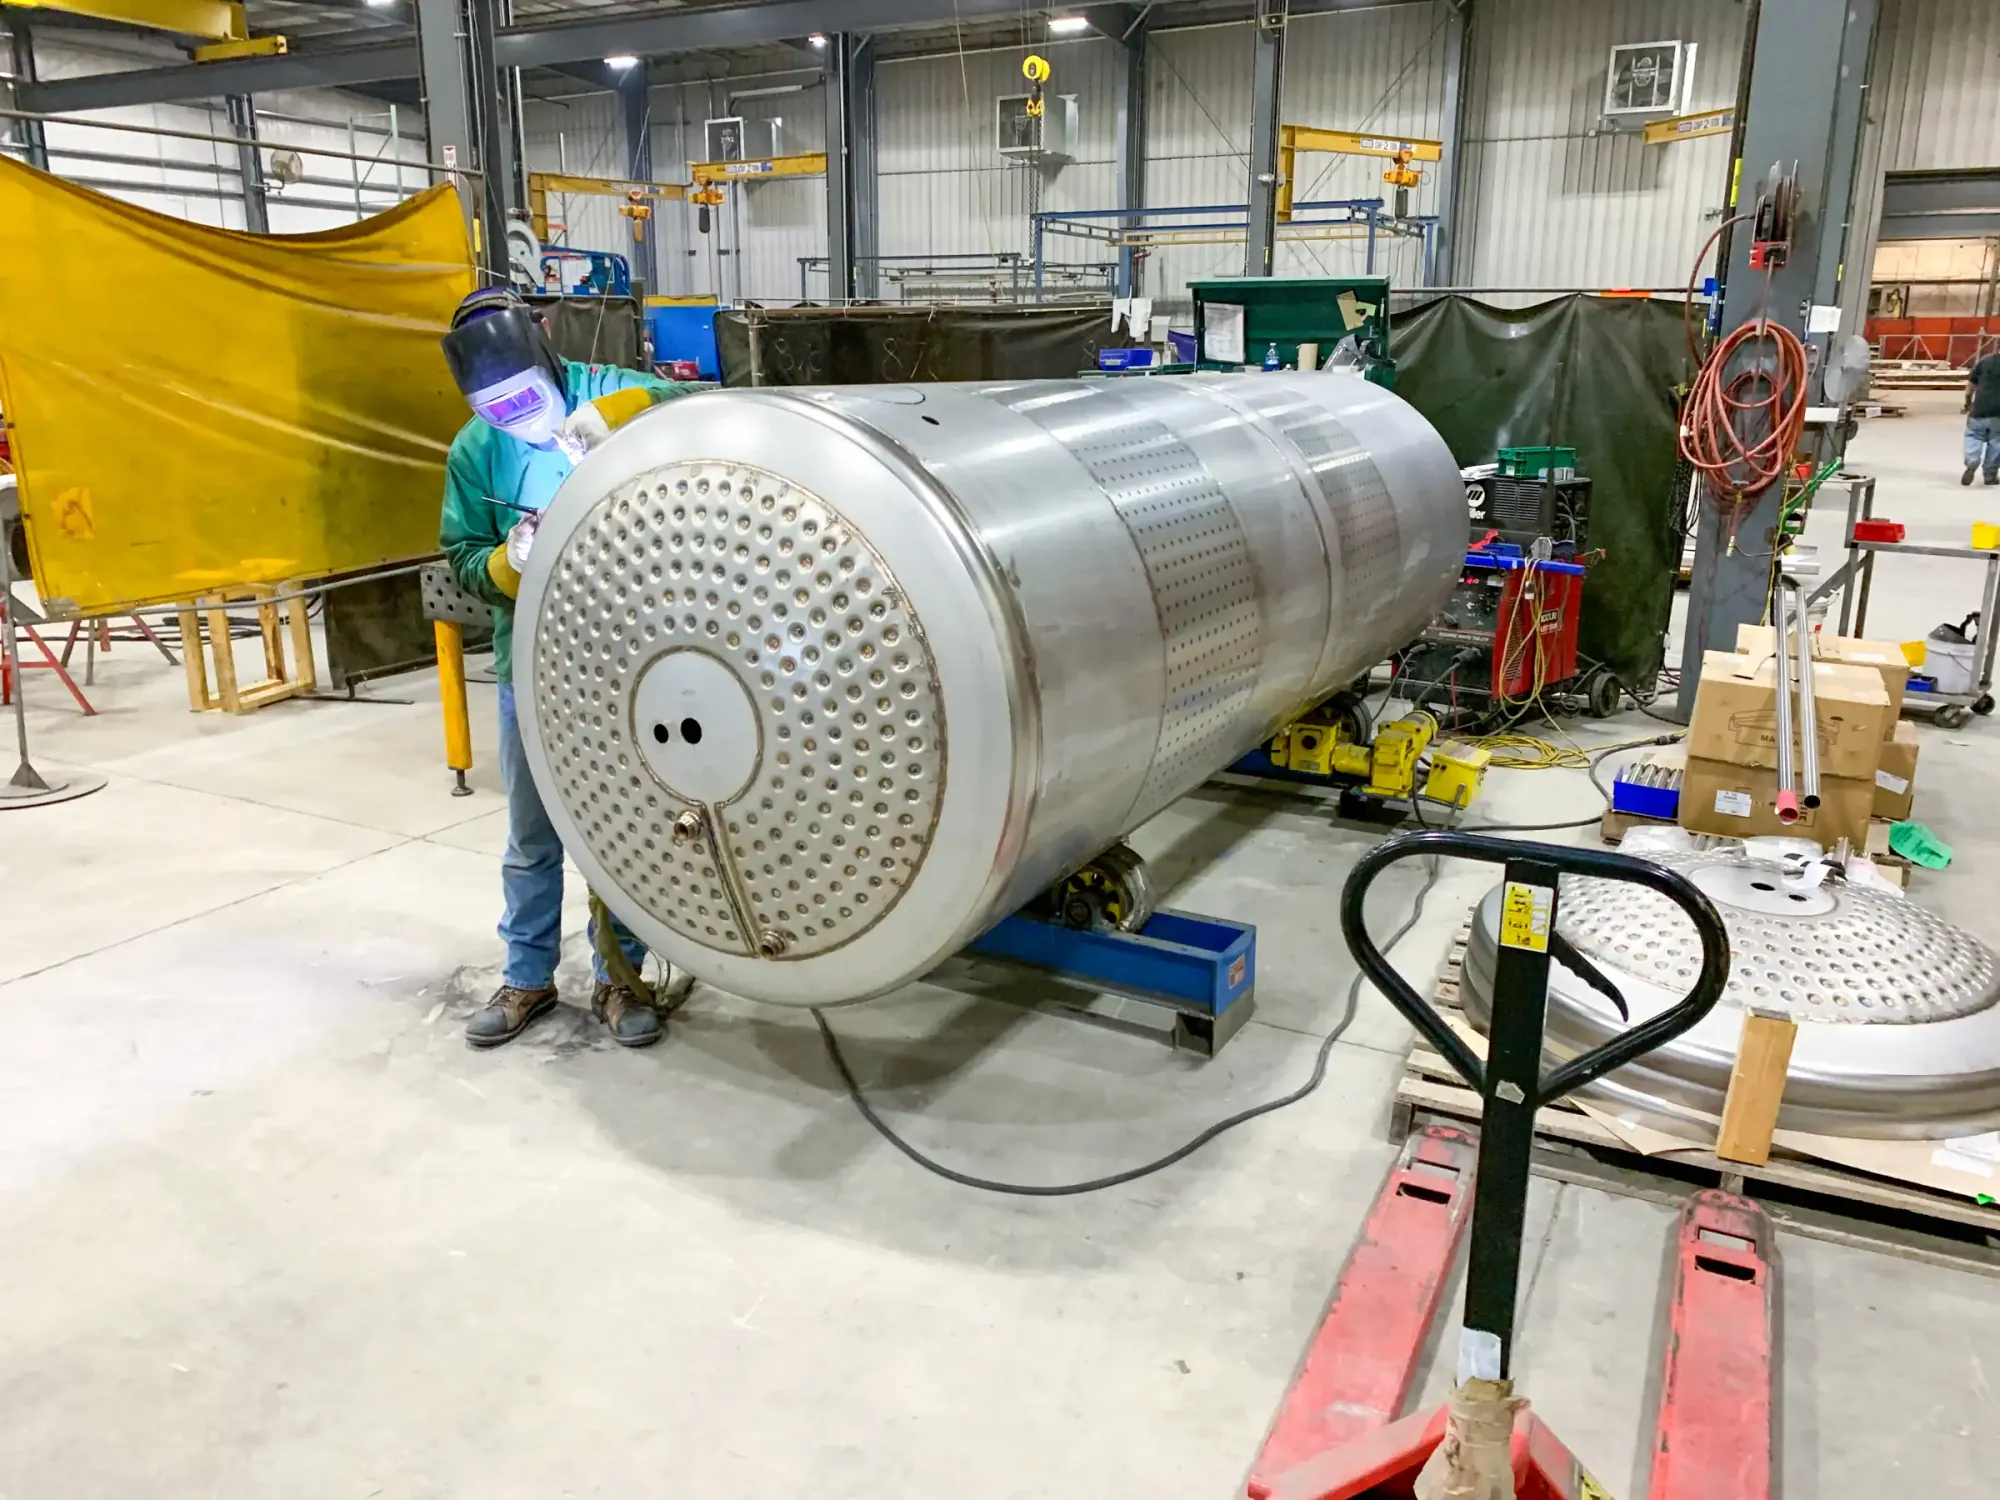
Agitator mounts, baffles, dimple or half-pipe jacketing, and reinforced top heads built to carry the loads your process puts on them. The mounting structure forms on our CNC press brakes and ties into the shell with full-penetration welds where the duty demands it. Tell us the agitator and drive details with the drawing so the mount and reinforcement are sized correctly.
Sanitary / Food-Grade Tanks
Tanks for food, beverage, and hygienic processing with crevice-free, full-penetration product-contact welds and interior surfaces finished to the Ra your spec calls out. Every wetted surface is pickled and passivated per ASTM A380 and A967, with copper sulfate verification when your specification or purchase order calls for it. When your drawing invokes 3-A or another hygienic design standard, the inspection points and turnover records are built around it.
Troughs, Hoppers, Chutes, and Replacements
- Troughs, hoppers, and chutes in heavy-gauge stainless and duplex
- Replacement tanks built from your existing drawings or reverse-engineered from the failed unit
One-Piece Shells, Fewer Seams
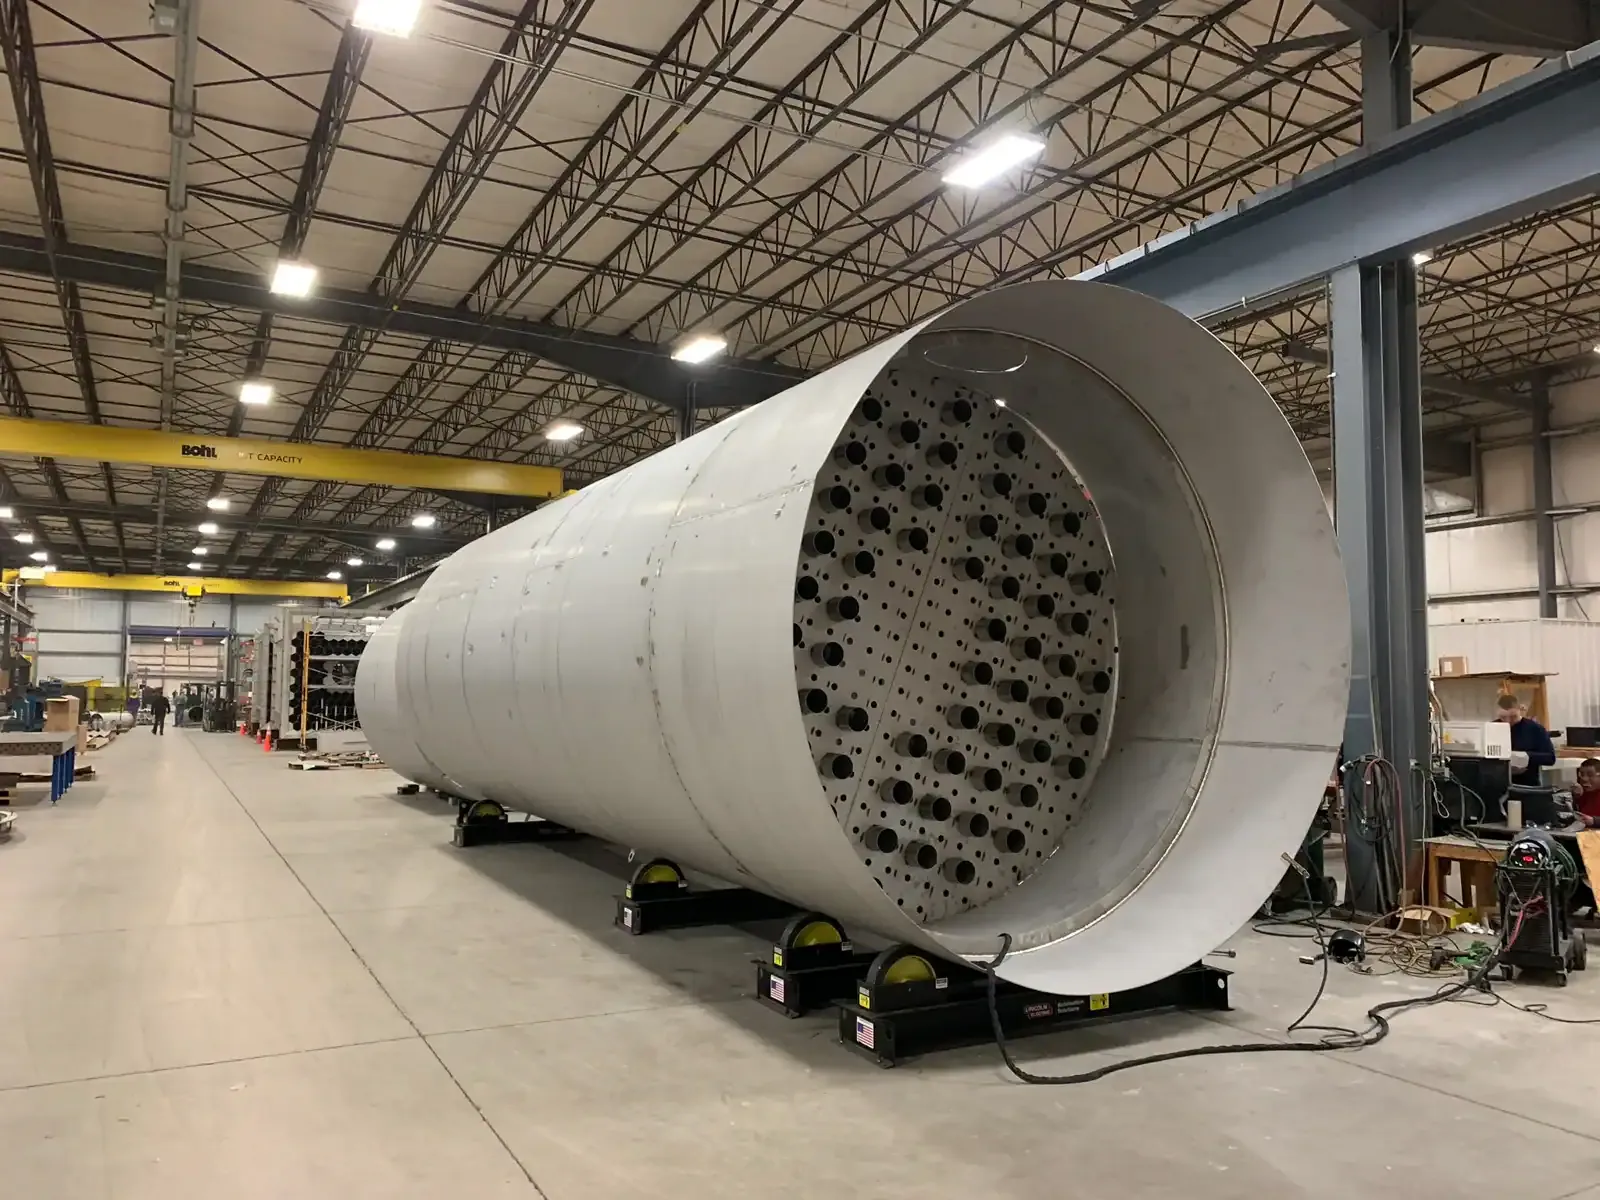
Rolling runs in the same building as cutting and welding, so a shell course comes off the roll and moves straight to fit-up without a freight leg between vendors. Where the geometry allows, we roll the cylinder in one piece instead of welding two formed halves. That removes a longitudinal seam, and every seam removed is a weld that cannot leak, distort during welding, or fail inspection.
The seams that remain are welded for the duty they carry. Long straight runs on austenitic stainless plate go to submerged arc for deposition rate and bead consistency. Straight seams on qualified stainless and duplex thicknesses are candidates for K-TIG, a single-pass full-penetration keyhole GTAW process that replaces multi-pass joints where the fit-up qualifies. Nozzles, manways, and interior product-contact welds run GTAW under ASME BPVC Section IX and AWS D1.6 procedures.
Scale is handled by sequencing rather than bravado. One of the longer wetted assemblies to ship from this floor, a 304L trough 100 feet end to end, was fabricated in laser-aligned sections with controlled heat input and held straight within 1/8 inch across the full span.
Forming the Rest of the Tank
Shells are half the bill of materials. Bases, stiffening rings, saddles, support legs, and mounting structures form on five CNC press brakes (two Trumpf TruBend 5320s, a TruBend 5230, a TruBend 5085S, and an Ermak), with heavy plate and long profiles bump formed in controlled increments. Blanks come off our flat lasers with bend allowances already in the flat pattern and weld prep on the edges that need it, so formed parts arrive at fit-up ready to tack.
Grades We Fabricate for Tanks
| Alloy | Why it gets specified | Welding notes |
|---|---|---|
| 304 / 304L | General storage, water service, the cost baseline | L grade on welded components |
| 316 / 316L | Chloride and chemical resistance; food, beverage, and pharma default | L grade prevents carbide precipitation |
| Duplex 2205 / 2507 | Roughly 2x the yield strength of 304; resists chloride stress cracking | Capped interpass, matching filler, ferrite checks |
| AL-6XN | Warm chloride and high-purity corrosive service | Overmatching nickel filler preserves resistance |
| Hastelloy C-276 / C-22 | Aggressive mixed-acid and reducing chemical service | Low heat input GTAW, tight bead control |
Most tank drawings arrive with the grade already specified, and we build to it. When the spec is open, the grade is a conversation we are glad to have during quoting: the right answer is the one that survives your product at the lowest total cost, not the most impressive name on the MTR, and we have talked more than one customer down from a nickel alloy a duplex would outlast. Either way, the value we add is the fabrication, holding the weld integrity and finish that make the grade perform in service.
Quality Verified Before It Ships
Every tank is inspected by our on-staff CWI, with NDE specified per the drawing and run under ASNT SNT-TC-1A Level III oversight: visual (VT), dye penetrant (PT) on root and product-contact welds, and ultrasonic (UT) on full-penetration joints as called out, with radiography (RT) coordinated through a qualified NDE partner when the spec requires it. PMI confirms alloy identity on specialty-metal work, and ferrite is measured on duplex production welds.
Finishing closes the loop. ASTM A380 pickling and A967 passivation in the 55-foot booth restore the passive layer on every weld and wetted surface. Copper sulfate verification is run and logged by lot and serial when your specification or purchase order calls for it. Drive-in booth access means most tanks go in whole, protecting fit-up tolerances and keeping the quality record against the as-built weldment.
Documentation for Your Tank
We can provide documentation as your purchase order and specification require:
- Material Test Reports (MTRs) traced by heat number from mill cert through finished weldment
- Weld maps identifying every joint, its WPS reference, and the welder stamp
- NDE reports (VT, PT, RT, UT as specified on the drawing)
- Ferrite measurement records for duplex welds
- Pickling and passivation certificate referencing ASTM A380 and A967, with copper sulfate verification records
- PMI records for specialty-alloy work
- Certificate of Conformance (CoC) to your purchase order
If your specification calls for a standard or a document we have not listed here, our quality department scopes it against the spec during quote review, before fabrication starts.