Hastelloy C-276, C-22 & AL-6XN Specialty Alloy Fabrication
We weld and form Hastelloy C-276, C-22, AL-6XN, and Alloy 31 to your engineering drawings, under ASME BPVC Section IX procedures for P43 nickel alloys and P45 super-austenitics, with 100% PMI at receiving and in-house pickling.
Capacity
60 +
AWS-certified welders
4
Specialty alloys qualified
100 %
PMI verified
1951
Fabricating since
Alloys we run
High-nickel and 6%-moly super-austenitic grades, built to your print
When 316L cannot survive concentrated acids, wet chlorides, or warm brine, engineers specify nickel-moly-chromium alloys like Hastelloy or super-austenitics like AL-6XN and Alloy 31. Each grade below runs under alloy-specific weld procedures, 100% incoming XRF PMI, and segregated carbon-free handling.
Versatile nickel-molybdenum-chromium alloy for reducing and oxidizing acids; qualified under ASME BPVC Section IX (GTAW, keyhole GTAW, pulse GMAW, PAW, and hybrid laser).
Enhanced resistance to localized pitting and mixed oxidizing-reducing acid streams compared with C-276, welded under ASME BPVC Section IX P43 procedures.
Bridges austenitic stainless and nickel alloys against warm chloride pitting and crevice attack; welded under ASME Section IX qualified procedures with overmatching Ni-Cr-Mo filler (ERNiCrMo-3 for standard service, ERNiCrMo-10 for severe chloride service).
Nitrogen-alloyed iron-nickel-chromium-molybdenum grade welded under ASME Section IX qualified procedures for hot sulfuric, phosphoric, and halide-bearing chemical streams.
Send your drawing, alloy UNS, and governing code so Quality can confirm WPS coverage.
Welding & Fabrication
Hot cracking, microsegregation, and sensitization are the real risks
Specialty alloys fail in the weld zone when a shop runs them like standard 304L. Procedures are matched to the metallurgy and governing code of each grade.
Narrow heat-input windows
Excess heat in Hastelloy promotes hot cracking and intermetallic precipitation; in AL-6XN it drives molybdenum microsegregation. Qualified procedures cap heat input pass by pass.
Low interpass temperature limits
Hastelloy C-276/C-22 and AL-6XN carry lower interpass ceilings than 300-series stainless. Welders verify interpass temperature before striking each subsequent pass.
Overmatching & alloy-matched fillers
AL-6XN welds with overmatching filler, ERNiCrMo-3 for standard service and ERNiCrMo-10 for severe chloride service, so the weld metal holds base-plate pitting resistance; C-276 and C-22 run heat-lot traced ERNiCrMo-4 and ERNiCrMo-10 fillers.
Forming, Rolling & Finishing
Built into tanks, skids, ductwork, and spools under one roof
High work-hardening rates and alloy-specific chemistry govern every step from plate rolling to final passivation.
High-tonnage forming & 5-axis cutting
Super-austenitic and nickel alloys work-harden rapidly. Five CNC press brakes and 5-axis laser trimming hold bend radii and nozzle cutouts to print.
Tanks, skids, ductwork & spools
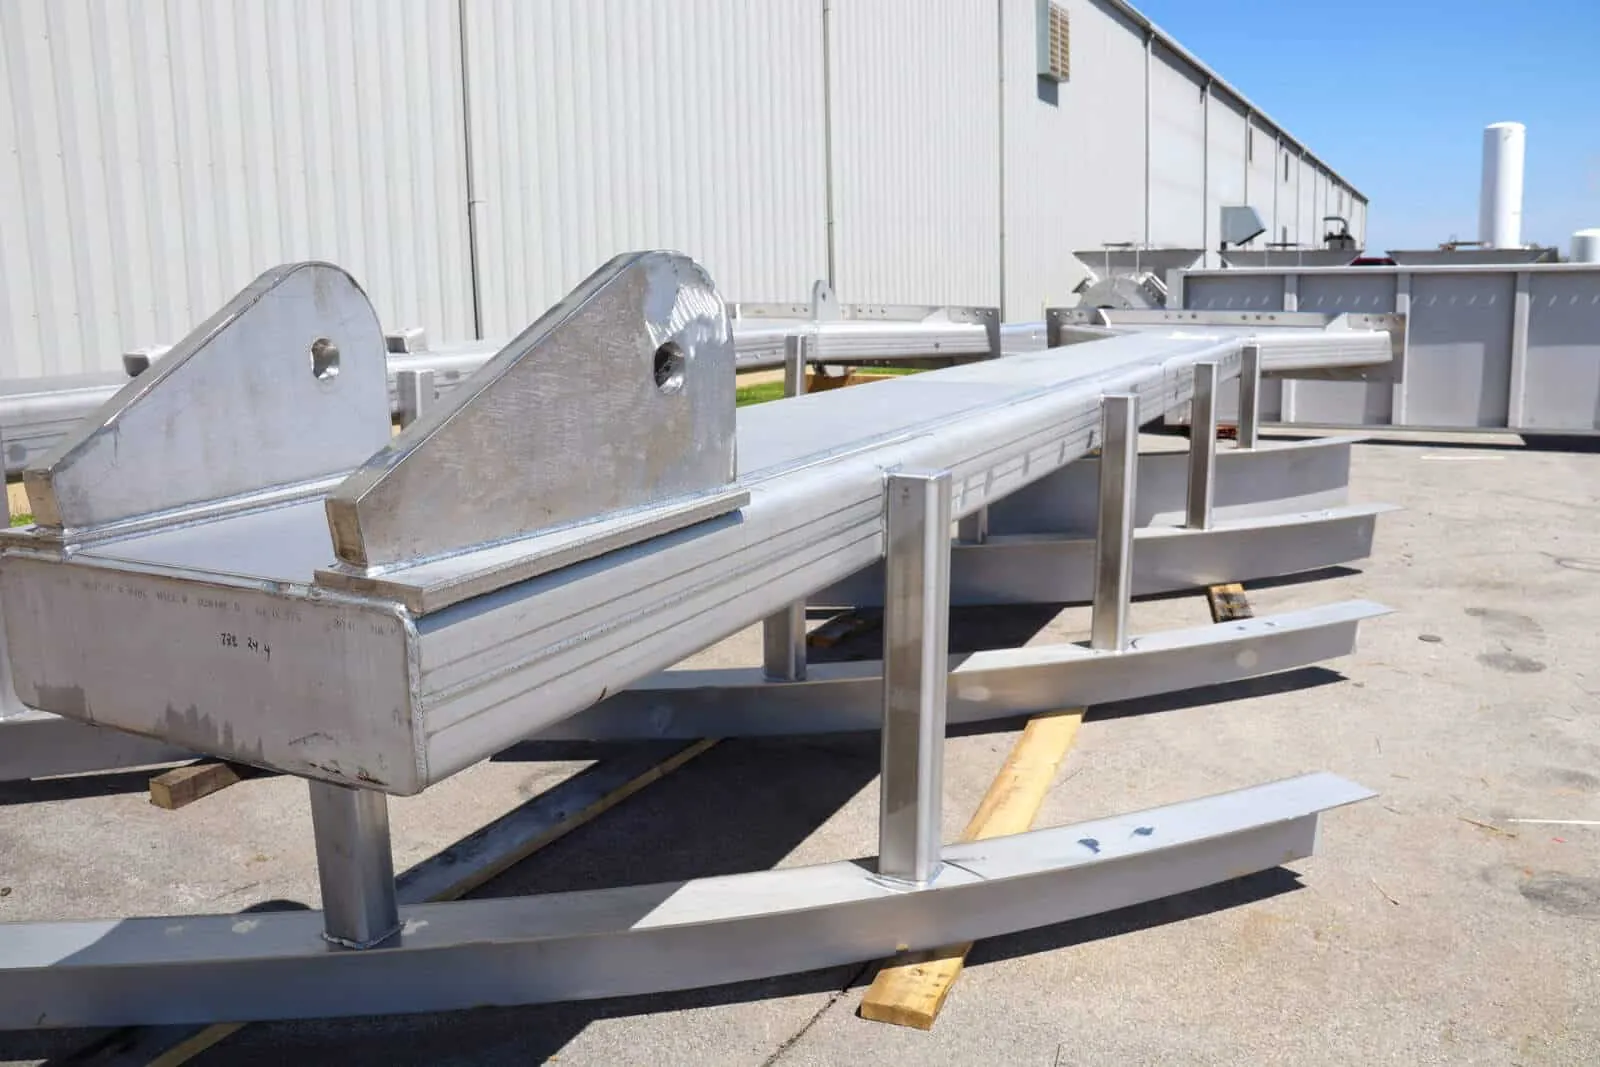
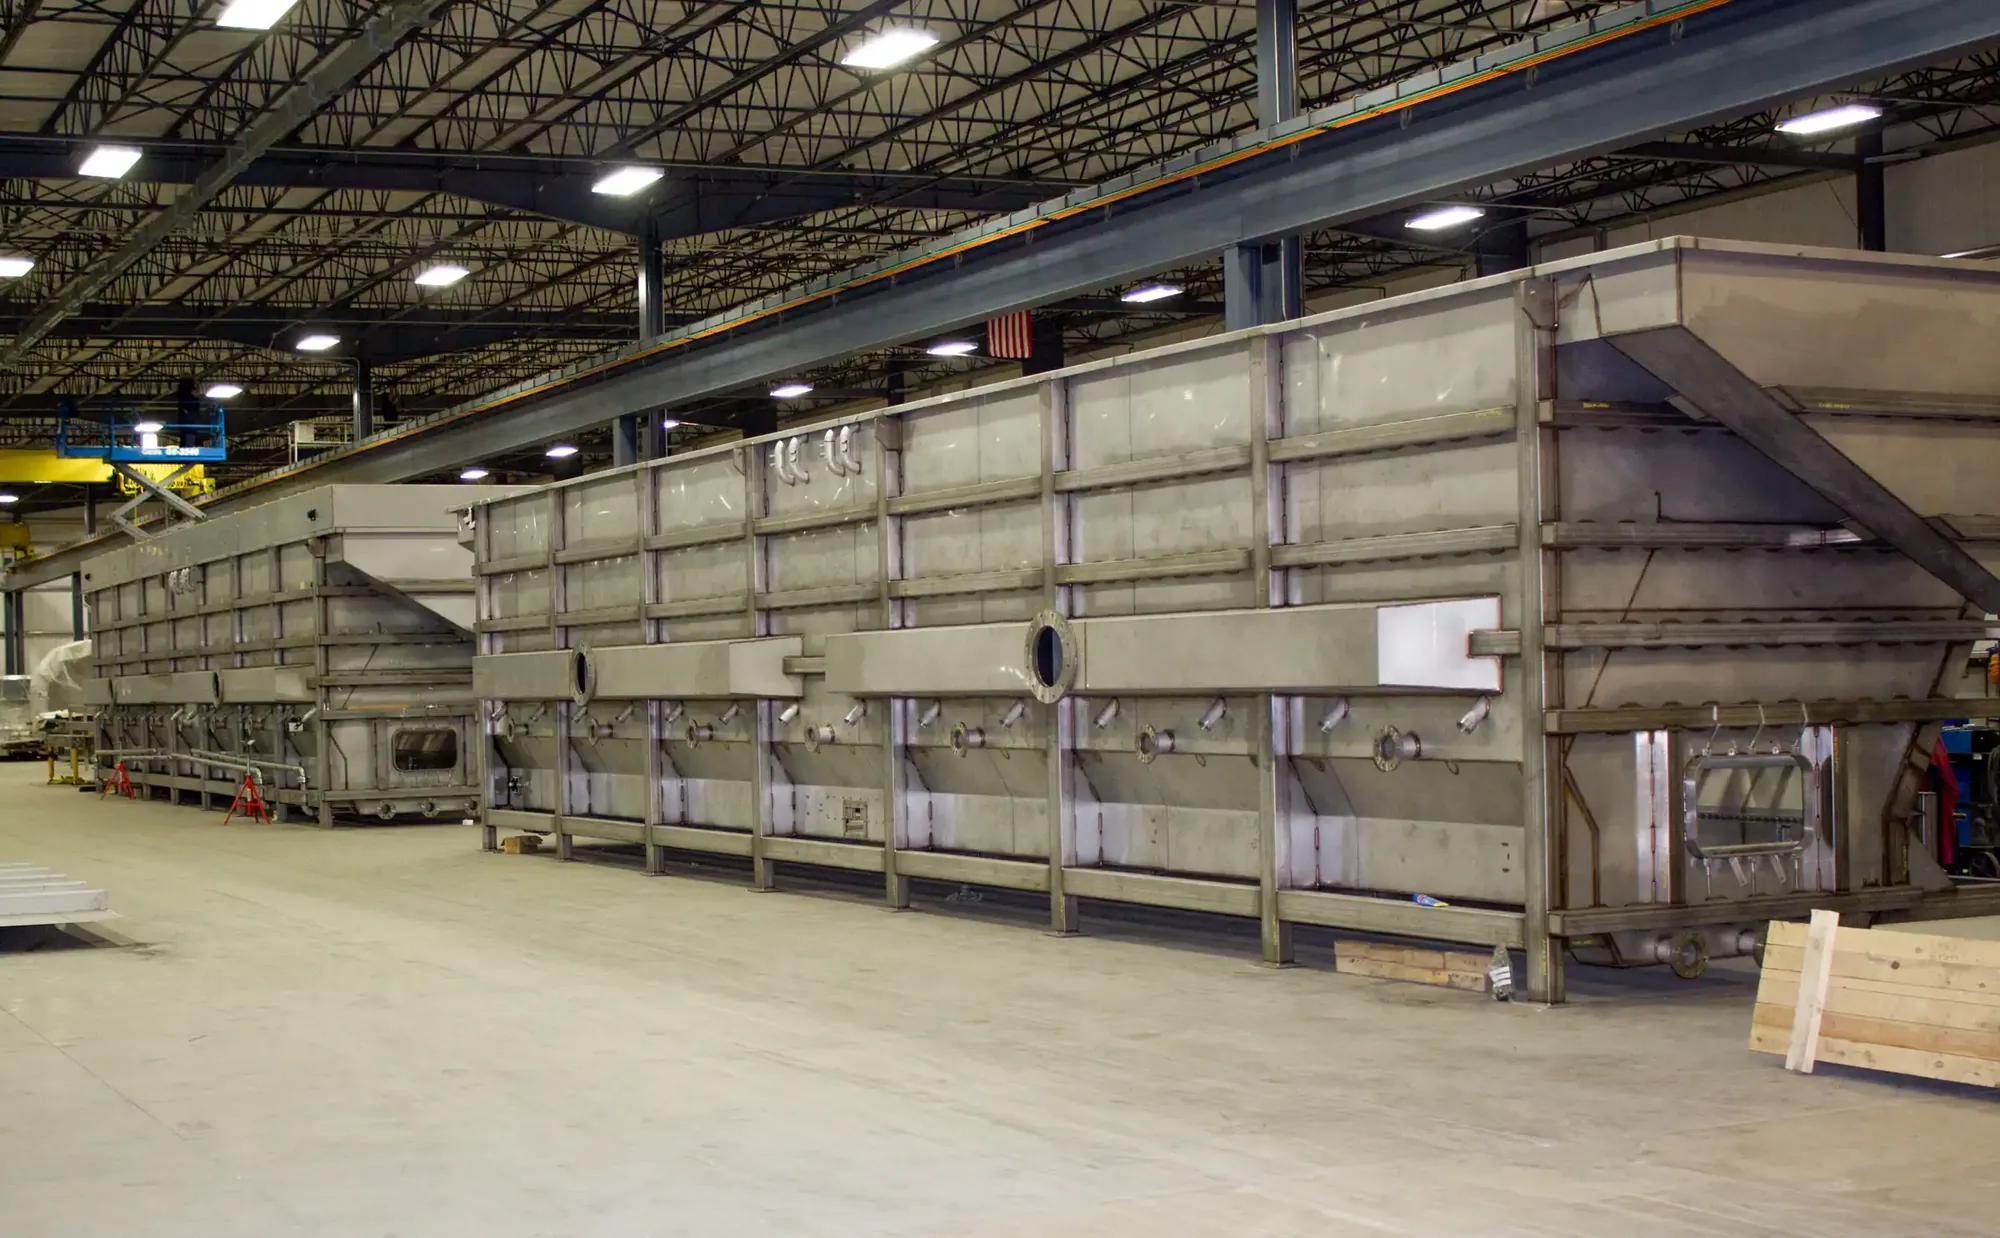
Hastelloy and AL-6XN plate and pipe fabricated into custom low-volume storage tanks, chemical skids, chloride ductwork, and process pipe spools.
Alloy-matched 55-foot pickling
In-house pickling and passivation per ASTM A380 and A967 in our 55-foot booth restores the passive layer using chemistry formulated for the specific alloy.
How We Build It Right
The alloy is only worth its cost if the welds hold
Paying mill premiums for C-276 or AL-6XN is wasted if iron contamination or an over-heated weld seeds crevice attack. We build to the grade your engineer specified inside controlled, carbon-free space.
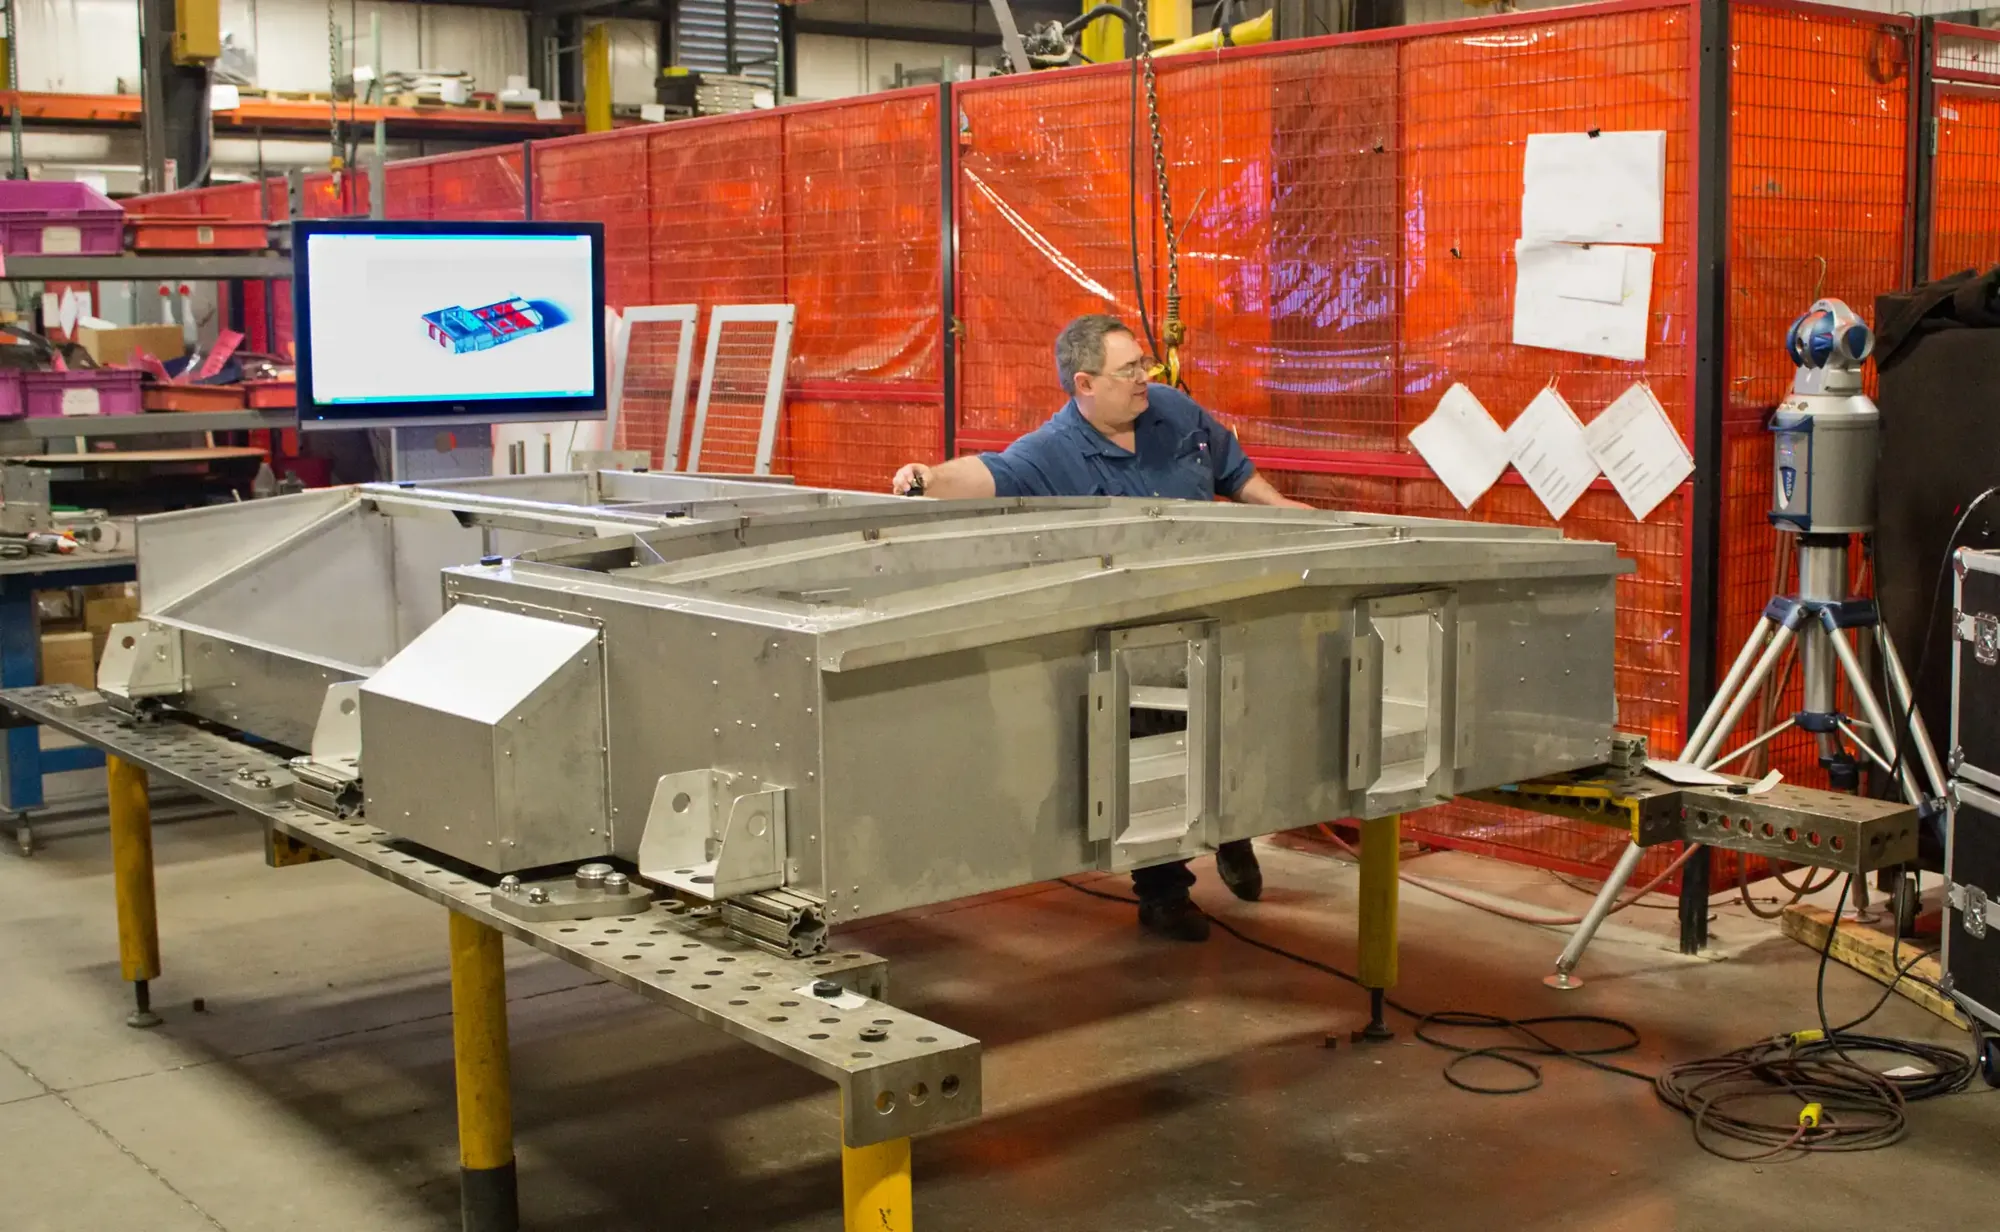
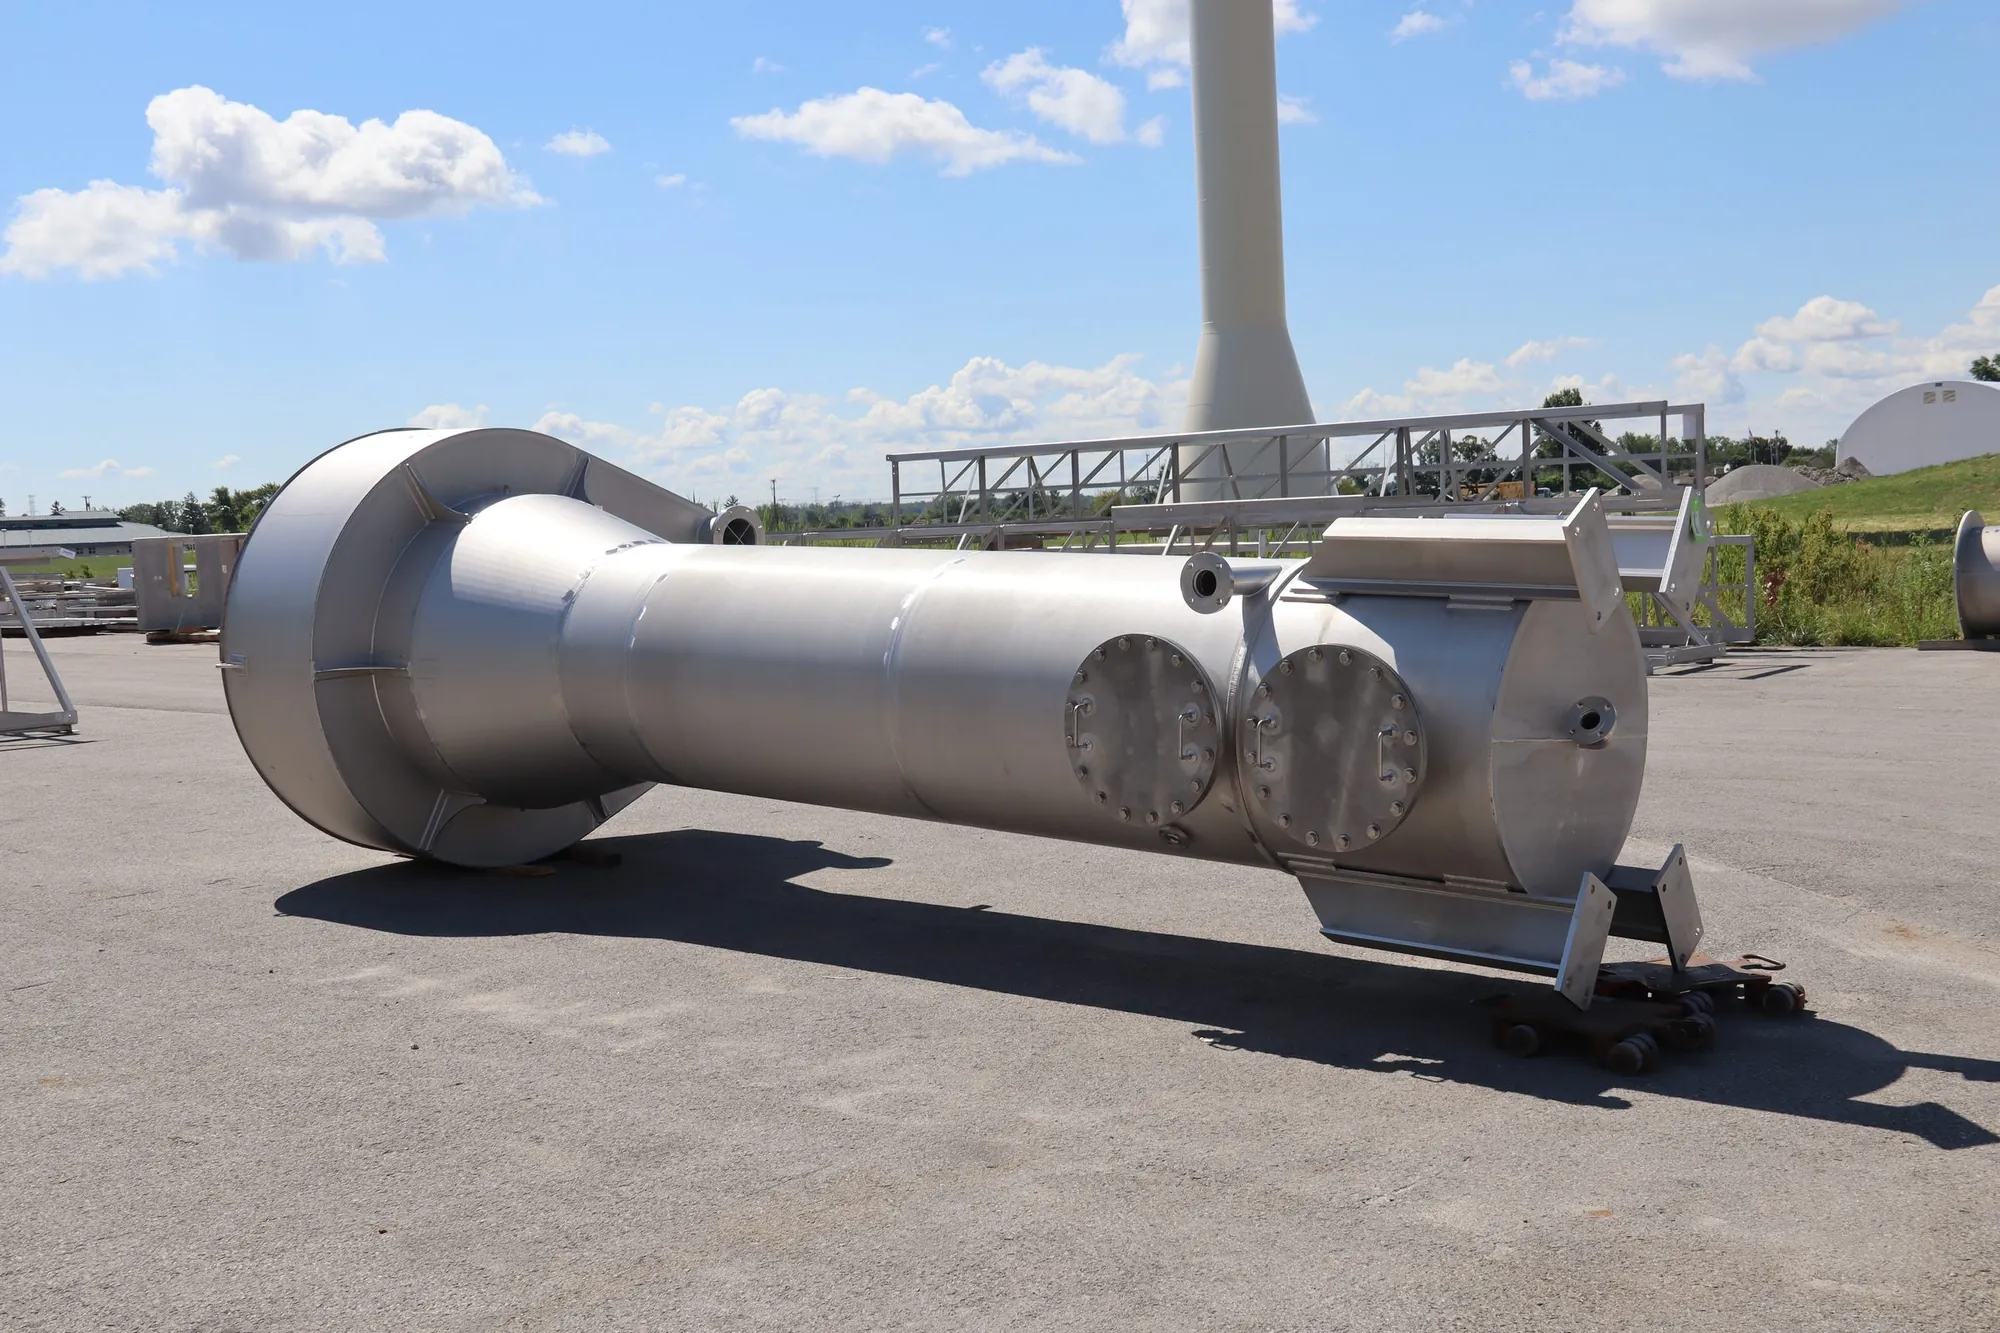
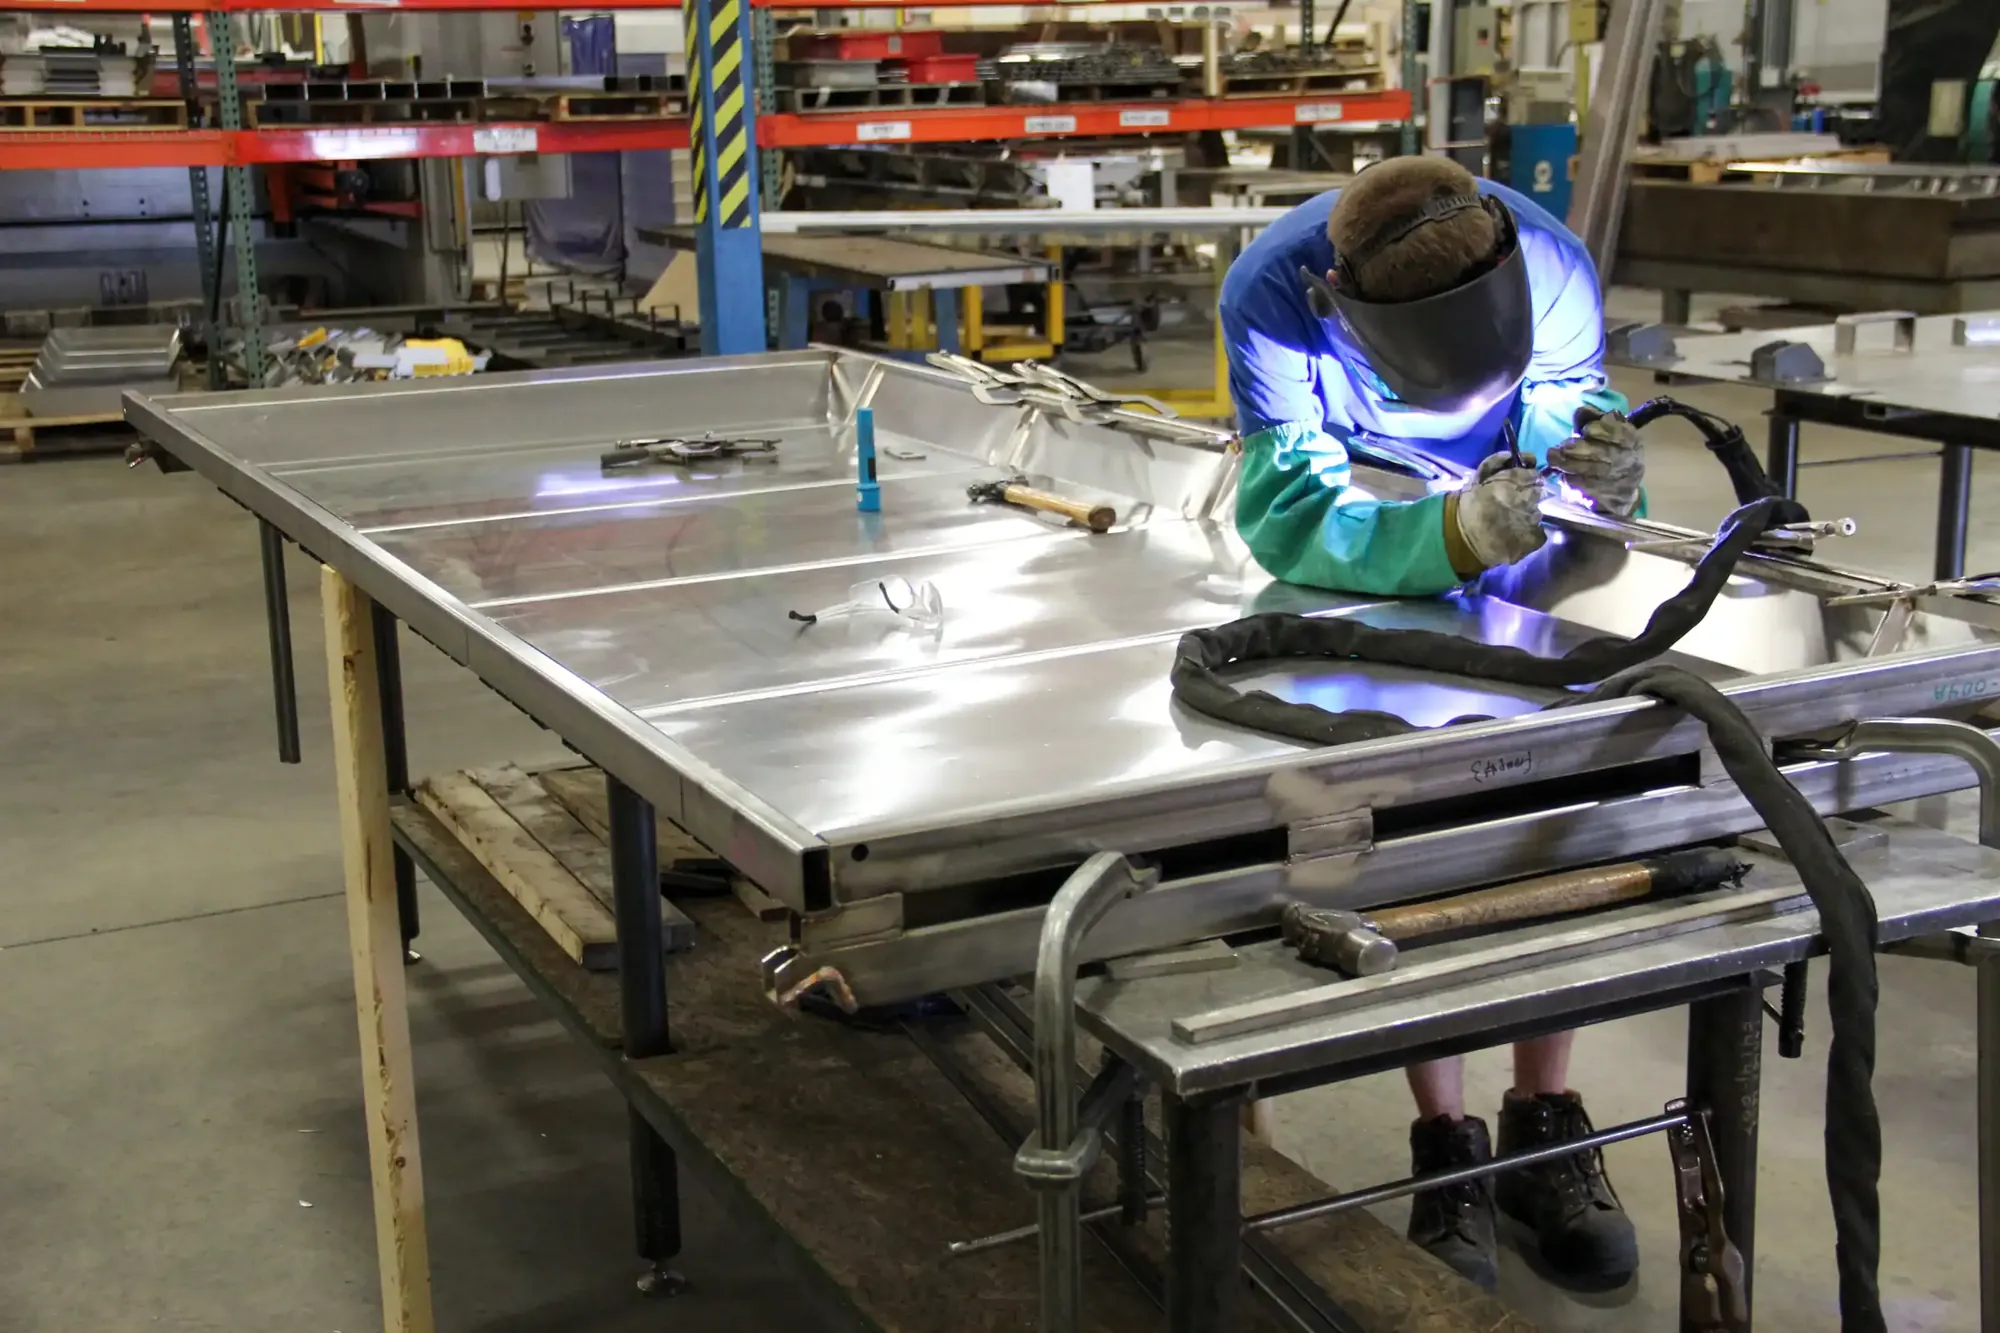
ASME BPVC Section IX procedures on P43 Hastelloy and on P45 AL-6XN and Alloy 31 prevent hot cracking and sensitization. On a pollution-control wet electrostatic precipitator in AL-6XN, we set row-to-row straightness before the first arc and held heat input low so the plate would not walk. See the build.
Specialty-alloy work runs inside our roughly 40,000 sq ft dedicated stainless-only production space, isolated from carbon steel, so embedded free iron cannot initiate pitting on wetted surfaces.
ISO 9001:2015 certified (#00157-4), with a CWI on staff and ASNT SNT-TC-1A Level III NDE oversight, providing the weld maps, MTR traceability, and inspection records your spec requires.
AL-6XN, Alloy 31, and Hastelloy C-276/C-22 are high-consequence grades where mix-ups are unacceptable. We log every heat under ISO 9001 controls and run 100% PMI at receiving before metal reaches a fixture.
Quality Assurance
Alloy-specific inspection points
Where It Runs
Industries that depend on specialty alloys
Where standard stainless is not enough: concentrated acids, chloride-rich solutions, and high-temperature chemical service.
Have a specialty alloy project on the board?
Other Materials We Fabricate
Back to the stainless families
Processes we run on this alloy
The in-house capabilities behind every build in this alloy, from laser cutting to final passivation.
Frequently asked questions
What engineers and procurement managers ask us about hastelloy c-276, c-22 & al-6xn specialty alloy fabrication.
How do you prevent hot cracking and sensitization in Hastelloy and AL-6XN?
With narrow heat-input control, low interpass temperatures, and overmatching or alloy-matched filler under qualified procedures: ASME BPVC Section IX, P43 for Hastelloy C-276 and C-22 and P45 for super-austenitics AL-6XN and Alloy 31. Nickel and 6%-molybdenum alloys lose corrosion resistance or crack if run hot, so the procedure governs the thermal window pass by pass.
When do engineers specify Hastelloy C-276 vs C-22 vs AL-6XN?
It tracks the process chemistry. Hastelloy C-276 (UNS N10276) handles strong reducing and oxidizing acids and wet chlorine. C-22 (UNS N06022) broadens resistance across mixed and oxidizing-reducing acid streams. AL-6XN (UNS N08367) is a 6% molybdenum super-austenitic specified for warm chloride pitting and crevice resistance in tanks, skids, ductwork, and piping. Most drawings arrive with the alloy locked; if your spec is open, send the media and temperature and we can advise.
Can you pickle and passivate Hastelloy and AL-6XN in-house?
Yes, with alloy-matched chemistry per ASTM A380 and A967 in our 55-foot drive-in booth. Standard stainless pickling parameters are not applied blindly to high-nickel or 6%-molybdenum alloys; the bath chemistry and dwell are matched to the alloy so weld scale is removed without attacking the base metal.
Can you fabricate ASME code piping or vessels in specialty alloys?
When your drawing calls for ASME code stamping, Northern holds the ASME PP stamp (Certificate #63198) for pressure piping fabrication and assembly and the ASME U stamp (Certificate #63199) for Section VIII Division 1 pressure vessel manufacture at our Oak Harbor, Ohio shop (Hartford Steam Boiler Authorized Inspection Agency). Send your drawing so Quality can verify active WPS code coverage for your alloy and thickness during quoting.
What documentation can you provide?
As your specification and purchase order require: Material Test Reports traced by heat, 100% XRF PMI records, weld maps with WPS references, NDE reports, and dimensional inspection records, available on request. Incoming PMI is standard on specialty-alloy work because 304L, 316L, AL-6XN, and nickel grades look identical on a rack.